 About Urh Social
 Terms of Service
 Privacy Policy
 Contact
How to Choose the Right CNC Toolpath Strategy for Different Machining Operations
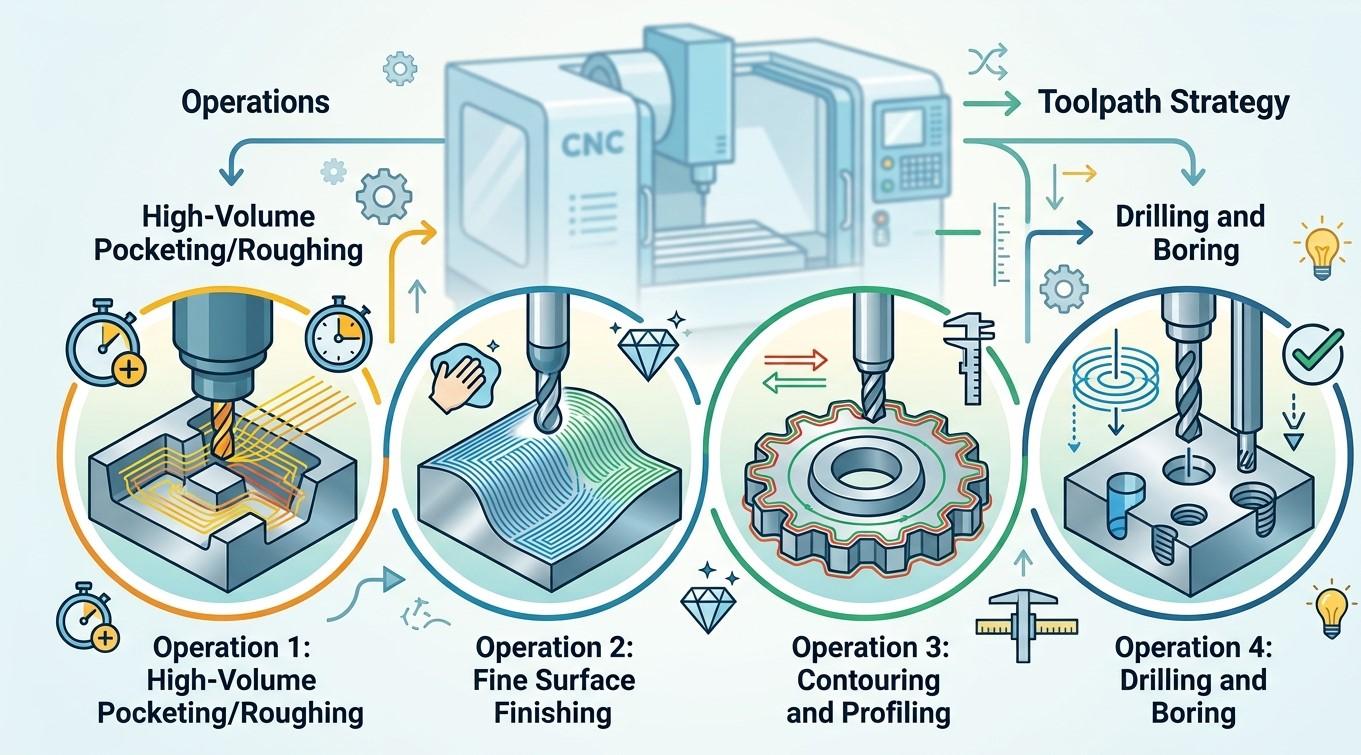
CNC machining depends on more than selecting the right machine and cutting tool. The CNC toolpath strategy also plays an important role in determining machining accuracy, surface finish, cutting efficiency, tool life, and production time. A well-planned toolpath controls how the cutting tool moves through the workpiece, how much material it removes, and how consistently cutting forces are applied. For manufacturers using CNC machining tools, selecting the appropriate strategy for each operation can improve productivity and reduce unnecessary tool wear. Khokhawala Trading LLC, an experienced Industrial Tools Supplier in Dubai, supports engineering, manufacturing, CNC machining, and industrial businesses with professional tooling and machining solutions.
What Is a CNC Toolpath Strategy?
A CNC toolpath is the programmed route followed by a cutting tool during machining. It determines the direction, speed, depth, and sequence of tool movements used to transform raw material into a finished component.
A toolpath strategy can influence:
- Material removal rate
- Cutting forces
- Tool engagement
- Surface finish
- Tool life
- Machining time
- Heat generation
- Chip evacuation
- Dimensional accuracy
- Machine stability
The ideal toolpath depends on the workpiece geometry, material, machining operation, cutting tool, machine capability, and required finish.
Why Toolpath Selection Matters
Choosing an unsuitable toolpath can increase machining time and tool wear while producing inconsistent results. In contrast, a suitable strategy can keep cutting conditions more stable and make better use of the cutting tool.
For example, a roughing operation usually requires efficient bulk material removal, while a finishing operation focuses more heavily on dimensional accuracy and surface quality. Using the same toolpath approach for both operations may not produce the best results.
Factors to Consider Before Choosing a Toolpath
Before selecting a CNC toolpath strategy, machinists should evaluate several factors.
Workpiece Material
Different materials generate different cutting forces and chip characteristics. Aluminum, mild steel, stainless steel, cast iron, titanium, and hardened materials may require different toolpaths and cutting conditions.
The selected industrial cutting tools should also be compatible with the workpiece material.
Part Geometry
Complex pockets, deep cavities, narrow slots, curved surfaces, holes, and thin walls can require different tool movements.
A toolpath that works well for an open flat surface may not be appropriate for a deep cavity or intricate 3D profile.
Cutting Tool
Tool diameter, flute count, cutting-edge geometry, tool material, and tool length all affect toolpath selection.
For example, carbide cutting tools can support demanding machining applications, but their performance still depends on suitable tool engagement and cutting parameters.
Machine Capability
The CNC machine's spindle speed, axis travel, rigidity, acceleration, and control capabilities should be considered before selecting an advanced toolpath strategy.
Required Surface Finish
Roughing and finishing require different approaches. A roughing toolpath prioritizes material removal, while a finishing strategy focuses on maintaining consistent engagement and producing the required surface quality.
Common CNC Toolpath Strategies
1. Face Milling Toolpath
Face milling is commonly used to create a flat reference surface on a workpiece.
The cutting tool moves across the top of the material while removing a controlled amount of stock.
A suitable face milling strategy should consider:
- Cutter diameter
- Radial engagement
- Step-over
- Cutting direction
- Workpiece size
- Surface finish requirements
Large-diameter face milling cutters can efficiently cover broad surfaces, while smaller tools may be required for restricted areas.
2. Pocketing Toolpath
Pocketing is used to remove material from enclosed or partially enclosed areas.
Common pocketing approaches include:
- Zig-zag machining
- Offset or contour-based passes
- Adaptive clearing
- Helical entry
- Trochoidal-style movement
For roughing deep pockets, maintaining controlled tool engagement can help reduce sudden cutting-force changes.
3. Adaptive Clearing
Adaptive clearing is a modern roughing strategy designed to maintain relatively consistent tool engagement.
Instead of taking large conventional cuts, the tool follows a controlled path that can efficiently remove material while limiting sudden changes in cutting load.
This strategy can be useful for:
- Deep pockets
- Complex cavities
- Hard materials
- High-efficiency roughing
- Large stock removal
When using adaptive strategies, tool rigidity, machine capability, and appropriate CNC tool holders remain important.
4. Contouring Toolpath
Contour machining follows the profile of a component.
It is commonly used for:
- External profiles
- Internal walls
- Steps
- Shoulders
- Curved boundaries
- Complex component outlines
Contour toolpaths are particularly useful during finishing because they allow the cutting tool to follow the desired geometry closely.
5. Slotting Toolpath
Slotting involves cutting a narrow channel across the workpiece, often using the full diameter of the tool.
Because the cutter may experience significant engagement, slotting can generate higher cutting forces than some lighter milling operations.
The machinist should consider:
- Tool diameter
- Flute count
- Material
- Slot depth
- Chip evacuation
- Spindle speed
- Feed rate
Using an unsuitable slotting strategy can increase heat, tool wear, and vibration.
6. Trochoidal Toolpath
Trochoidal machining uses controlled circular or looping movements while gradually advancing through the material.
This can reduce the amount of radial engagement compared with conventional full-width slotting.
Trochoidal strategies can be useful when machining:
- Narrow slots
- Hard materials
- Deep cavities
- Difficult-to-machine alloys
They can also help manage heat and cutting forces when correctly programmed.
7. Helical Toolpath
A helical toolpath moves the cutting tool gradually around a circular path while simultaneously moving along the Z-axis.
It is commonly used for:
- Hole interpolation
- Circular pockets
- Bore machining
- Ramping into material
Helical entry can provide a smoother way to introduce the tool into the workpiece compared with plunging directly into solid material.
8. 3D Surface Machining
Complex components often require 3D toolpaths to machine curved surfaces.
Common strategies include:
- Parallel finishing
- Scallop machining
- Waterline machining
- Pencil milling
- Constant-stepover finishing
- Morphing toolpaths
The appropriate strategy depends on surface geometry and the required finish.
For complex molds and dies, combining multiple strategies may produce better results than relying on one toolpath for the entire component.
Choosing Toolpaths for Roughing Operations
Roughing focuses on removing material efficiently while leaving controlled stock for finishing.
A good roughing strategy should:
- Remove material efficiently
- Control cutting forces
- Maintain suitable tool engagement
- Provide effective chip evacuation
- Avoid unnecessary tool movement
- Protect the cutting edge
Adaptive clearing, pocket roughing, and controlled step-over strategies are often useful for high-volume material removal.
Tool selection is equally important. A rigid cutter and suitable CNC machining tools can improve stability during heavy roughing operations.
Choosing Toolpaths for Finishing
Finishing operations focus on achieving the required dimensions and surface quality.
Finishing strategies may include:
- Contour passes
- Parallel passes
- Scallop machining
- Pencil passes
- Fine step-over passes
- Surface-following toolpaths
The required step-over should be considered carefully. A smaller step-over can improve surface quality but may increase machining time.
The final strategy should balance surface requirements with production efficiency.
Toolpath Selection for Different Materials
Aluminum
Aluminum generally benefits from efficient chip evacuation and tooling designed to reduce built-up edge.
Toolpaths should avoid unnecessary rubbing and excessive heat generation.
Steel
Steel machining requires careful control of cutting forces and tool engagement. Stable roughing and finishing strategies can help maintain tool life.
Stainless Steel
Stainless steel can generate significant heat and may work harden under unsuitable machining conditions. Controlled engagement and appropriate cutting tools are important.
Cast Iron
Cast iron can produce abrasive chips and may generate significant dust. Tool selection, cutting conditions, and chip management should be considered carefully.
Hardened Materials
Hardened materials often require rigid setups, appropriate carbide or advanced cutting tools, controlled engagement, and suitable finishing strategies.
The Role of Tool Holding in Toolpath Performance
A toolpath can be correctly programmed but still produce poor results if the cutting tool is not held securely.
Quality CNC tool holders help provide:
- Better rigidity
- Reduced runout
- Improved repeatability
- More stable cutting
- Better surface finish
Tool overhang should also be minimized wherever possible. Excessive tool extension can increase deflection and vibration, especially during deep machining.
Before production, operators should inspect the holder, tool shank, collet, and spindle interface for contamination or damage.
How Toolpath Strategy Affects Tool Life
Tool life is strongly influenced by how the cutting edge engages with the workpiece.
A suitable toolpath can help prevent:
- Excessive cutting forces
- Sudden tool engagement
- Excessive heat
- Uneven tool loading
- Chatter
- Premature edge wear
Combining the right toolpath with suitable carbide cutting tools, correct cutting parameters, and proper coolant delivery can help create a more predictable machining process.
Using Toolpaths to Improve Surface Finish
Surface finish is influenced by tool geometry, cutting parameters, toolpath direction, step-over, machine rigidity, and tool condition.
For finishing operations, machinists should consider:
- Tool diameter
- Nose radius or ball-nose geometry
- Step-over
- Feed rate
- Cutting direction
- Tool runout
- Machine vibration
- Workholding rigidity
Precision measuring tools can be used after machining to verify that the component meets dimensional and quality requirements.
Common CNC Toolpath Mistakes
Several common mistakes can reduce machining performance.
Using One Strategy for Every Operation
Roughing, semi-finishing, and finishing have different objectives. Each should be planned accordingly.
Excessive Tool Engagement
Large engagement can increase cutting forces, heat, and tool wear.
Ignoring Tool Overhang
Long tools can deflect, especially during deep machining.
Poor Chip Evacuation
Accumulated chips can cause recutting, heat buildup, surface damage, and premature tool wear.
Choosing Toolpaths Without Considering Machine Capability
Advanced toolpaths require suitable CNC machine dynamics and control capabilities.
Ignoring Measurement
Even a well-designed toolpath must be verified through dimensional inspection and process monitoring.
Best Practices for CNC Toolpath Selection
For consistent CNC machining performance, workshops should follow a systematic approach:
- Analyze the part geometry before programming.
- Identify the workpiece material.
- Select suitable industrial cutting tools.
- Choose a roughing strategy for efficient stock removal.
- Use appropriate semi-finishing and finishing strategies.
- Minimize tool engagement where practical.
- Reduce unnecessary tool overhang.
- Use rigid CNC tool holders.
- Optimize speed, feed, depth, and step-over.
- Ensure effective chip evacuation.
- Monitor tool wear throughout production.
- Verify finished dimensions using precision measuring tools.
This approach can help improve machining consistency while reducing unnecessary production costs.
Benefits of Choosing the Right CNC Toolpath Strategy
An appropriate toolpath strategy can provide several operational benefits:
- Faster material removal
- Reduced machining time
- Improved tool life
- Better surface finish
- More consistent dimensions
- Lower cutting forces
- Reduced vibration
- Improved chip evacuation
- Greater production efficiency
- Reduced scrap and rework
The biggest benefit comes from treating the toolpath, cutting tool, machine, workholding, and cutting parameters as one integrated machining system.
Conclusion
Selecting the right CNC toolpath strategy is an important part of achieving efficient, accurate, and repeatable machining results. Face milling, pocketing, adaptive clearing, contouring, slotting, trochoidal machining, helical movements, and 3D finishing strategies each have specific applications. The correct choice depends on the workpiece material, component geometry, cutting tool, machine capability, required surface finish, and production objectives.
Using appropriate industrial cutting tools, CNC machining tools, carbide cutting tools, and reliable CNC tool holders can help maximize the benefits of a well-planned toolpath. Regular inspection with precision measuring tools also helps verify machining accuracy and identify problems before they affect production.
For businesses seeking dependable tooling and machining solutions, Khokhawala Trading LLC is an experienced Industrial Tools Supplier in Dubai, providing professional industrial tools, CNC tooling, machining accessories, and measurement solutions for manufacturing and engineering applications.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Portuguese (Brazil)
 Greek